Inquiry
Form loading...
-
Phone
-
E-mail
-
Whatsapp
-
WhatsApp
High-grade sealing fittings meticulously manufactured to protect sensitive telecom boards, RF units, and optical splitters from moisture, extreme thermal swings, and chemical contaminants.
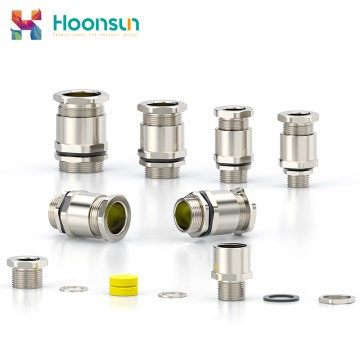
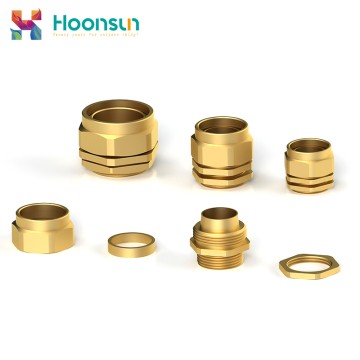
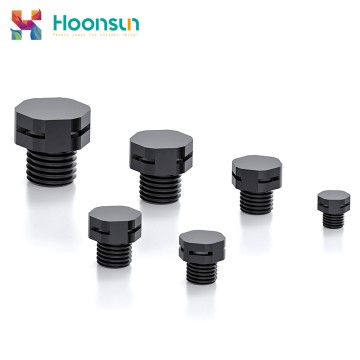
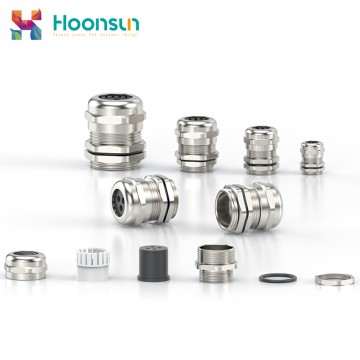
An in-depth analysis of structural integrity, composite material formulation, and engineering criteria for modern outdoor telecommunication housings.
With the aggressive rollout of massive MIMO antennas, Remote Radio Units (RRU), and Active Antenna Units (AAU), high-frequency wireless equipment generates greater internal heat while facing severe weather. Reinforced nylon cable glands offer superior non-conductive safety, non-interference with RF signals, and stable thermal dissipation.
Outdoor telecom cabinets operate in continuous sunlight, coastal saline mist, and fluctuating acid rain conditions. By utilizing PA66 reinforced with glass fiber and specialized UV stabilizers, nylon reinforced glands eliminate galvanic corrosion while delivering UL 94 V-0 flame retardancy and IP68 watertight longevity.
Modern telecom enclosures combine DC power feeds and high-density multi-core optical cables. The elastic clamping jaw and high-recovery NBR/EPDM sealing ring provide constant clamping force, effectively preventing fiber micro-bending attenuation and cable slippage during high-velocity wind loads.
In the telecommunication infrastructure ecosystem, outdoor cabinets, fiber distribution hubs (FDH), and optical line terminal (OLT) enclosures operate as the nerve centers of data transmission. These enclosures face severe environmental stressors including ambient temperature variations from -40°C to +100°C, solar ultraviolet degradation, persistent humidity, and mechanical vibrations caused by wind and traffic. A failure in the cable penetration point compromises the entire internal active matrix, causing costly network downtime, corrosion of printed circuit boards, and signal loss.
Polyamide (Nylon 66) reinforced with precision-engineered additive matrices stands as the standard of excellence for non-metallic cable glands in the telecommunications sector. Compared to unreinforced plastics, glass-fiber-reinforced nylon delivers elevated tensile strength, creep resistance under sustained mechanical tension, and dimensional stability across prolonged operational lifespans exceeding 20 years.
As micro-edge data centers and FTTH (Fiber to the Home) splitters multiply in urban and rural environments, cable gland designs are adapting toward ultra-compact footprints and multi-hole configurations. Future iterations are integrating intelligent monitoring sensors capable of assessing gasket pressure degradation and environmental humidity within the gland body, signaling preventative maintenance schedules before an environmental breach occurs.
Zhejiang Hongxiang Connector Co., Ltd.
Founded in 2006, Zhejiang Hongxiang Connector Co., Ltd. is rooted in Yueqing, Zhejiang — a national hub for precision electrical manufacturing in China. After nearly two decades of dedicated development, the company has evolved into a large modern industrial connectivity solutions provider integrating R&D and design, large-scale intelligent manufacturing, global sales, and one-stop services. It stands as a benchmark enterprise of considerable scale and influence in China’s cable gland and connector industry, and a key player among national high-tech enterprises.
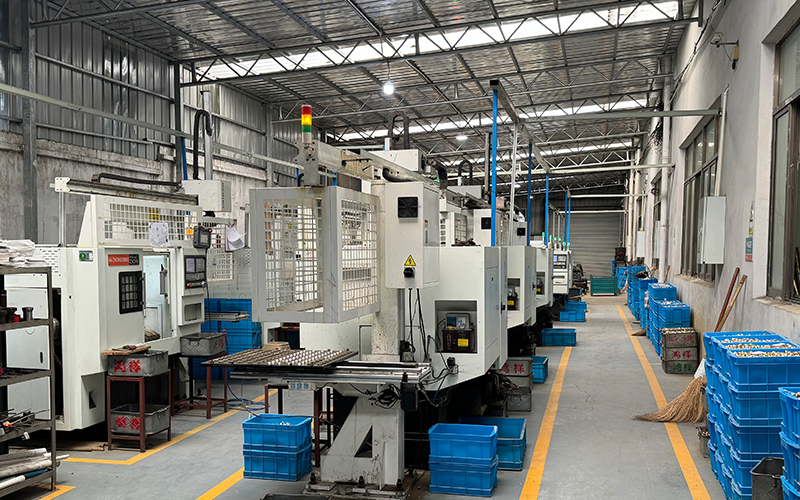
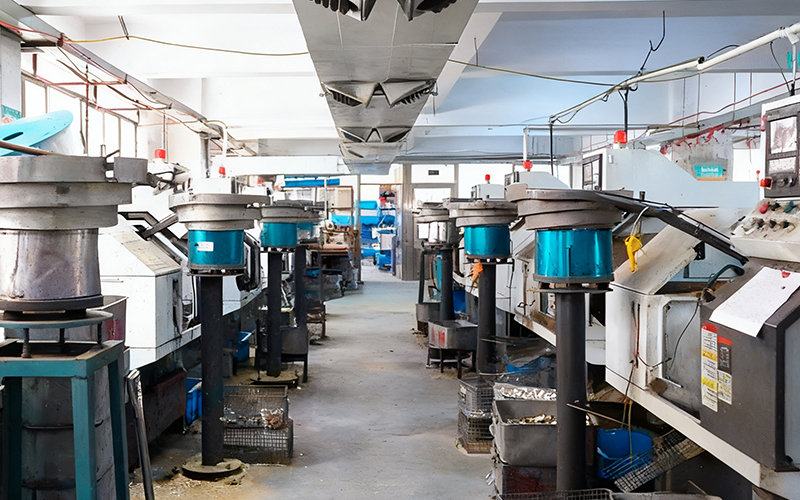
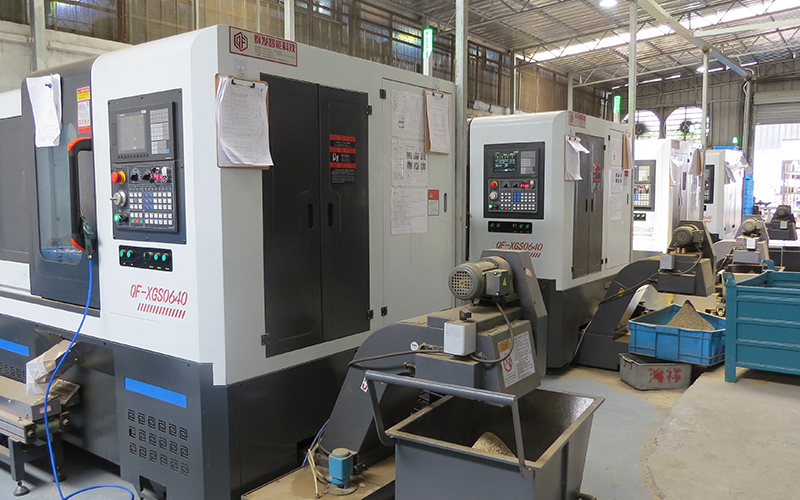
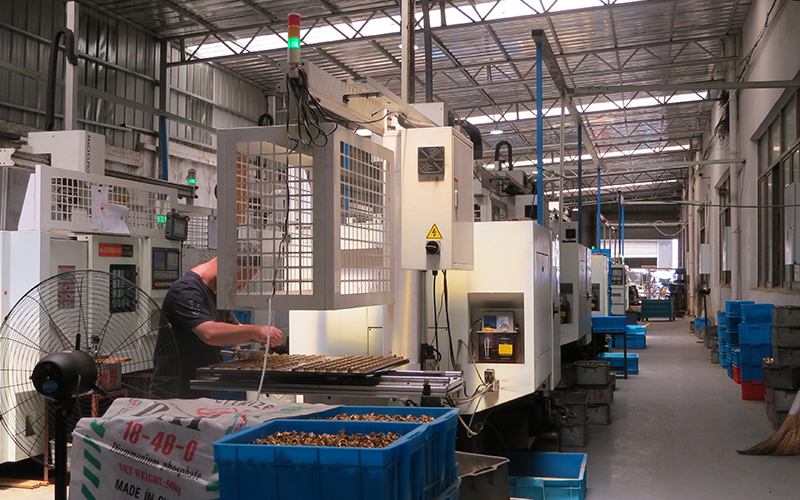
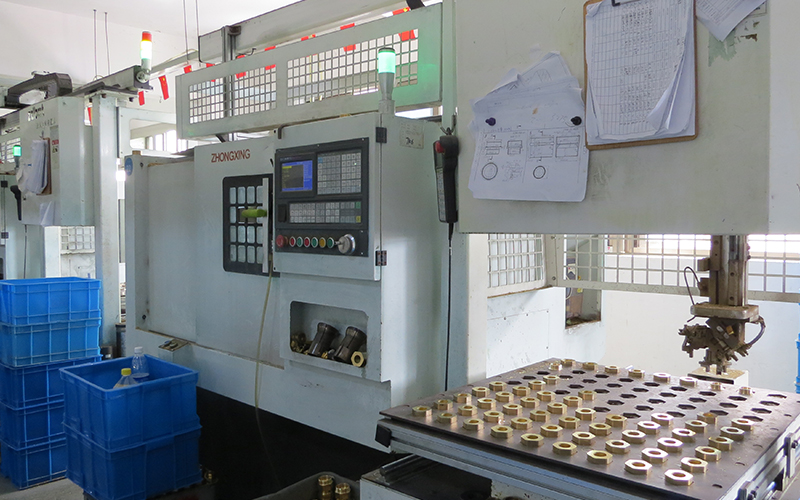
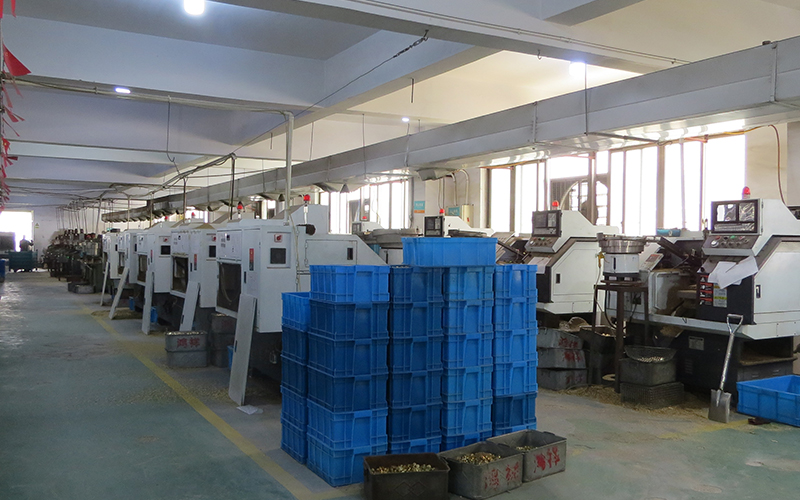
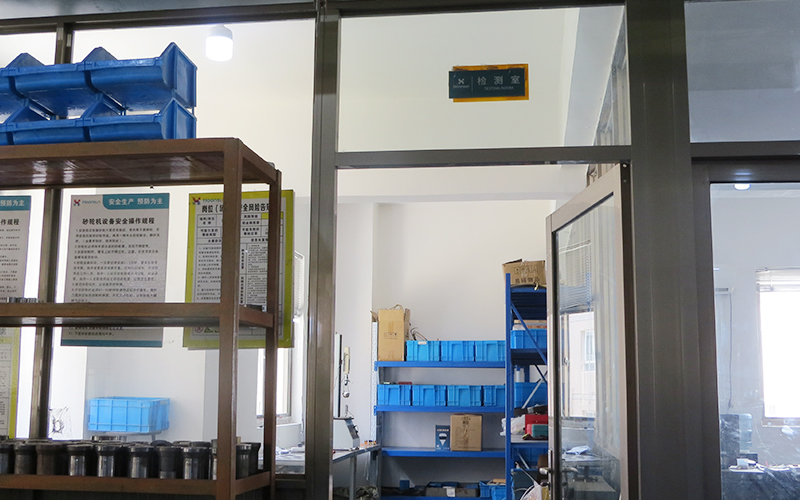
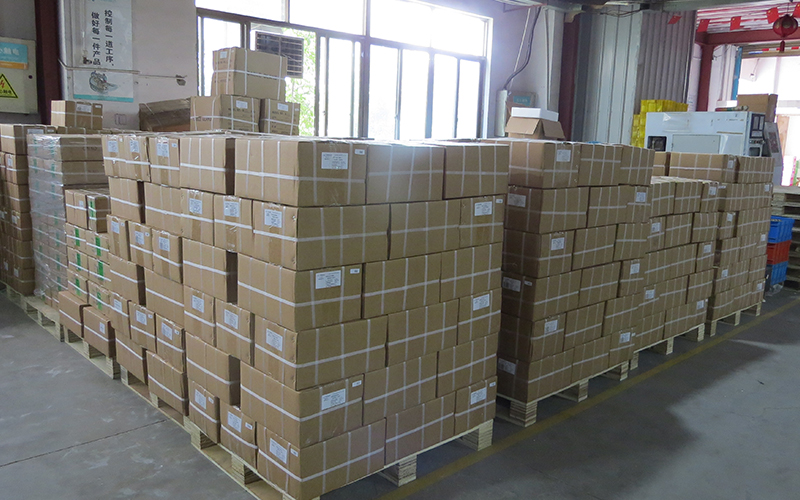
Boasting a modern intelligent manufacturing industrial park, the company operates a standardized production workshop of over 10,000 square meters, equipped with multiple high-precision automated production lines, CNC machining centers, and a full-process quality control laboratory, establishing an industry-leading large-scale manufacturing system. With a core team of more than 300 professionals — over 30% of whom are R&D and quality management personnel — its annual production capacity exceeds 80 million units. The company is fully capable of handling large-volume orders, urgent custom projects, and long-term strategic supply partnerships for domestic and international clients, ranking among the industry’s top tier in both production capacity and delivery efficiency.
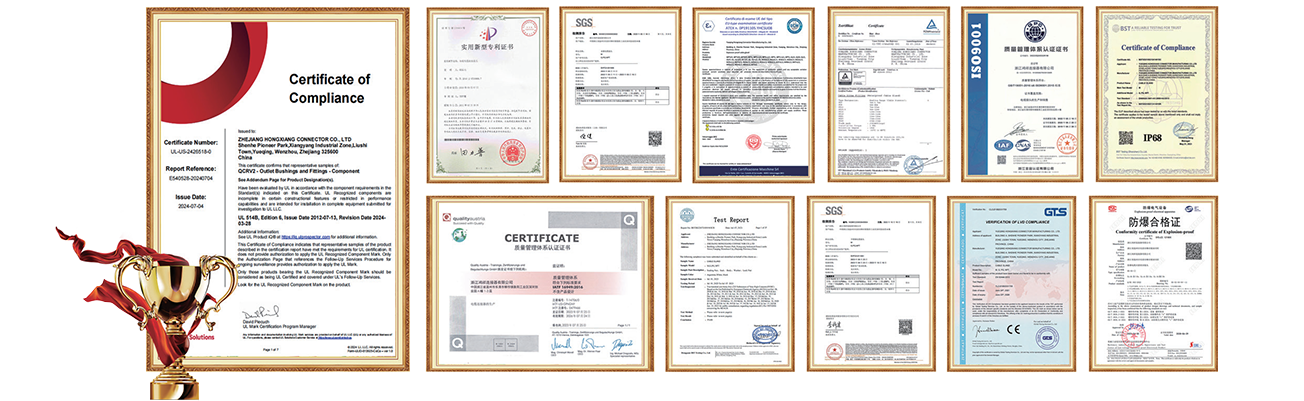
Its core product portfolio includes metal cable glands, nylon cable glands, waterproof cable glands, explosion-proof connectors, conduit fittings, and various customized connecting accessories. These products serve high-end sectors such as industrial electrical equipment, new energy equipment, rail transit, shipbuilding and heavy industry, construction machinery, military supporting facilities, and communication & industrial control. Adhering to stringent manufacturing standards and uncompromising quality requirements, the company has obtained a series of internationally recognized certifications, including ISO9001, IATF16949 automotive quality management system, CE, UL, ATEX explosion-proof certification, RoHS, and IP68 high-protection rating. Its core technologies and product performance have reached international advanced levels, with nearly 100 invention and utility model patents to its name, continuously driving technological upgrading across the industry.
Continuous investment in precision tooling, global standard certifications, and state-of-the-art polymer manufacturing since 2006.
Every cable gland and venting accessory meets uncompromising safety, flame retardance, and ingress verification (UL, IP68, CE, ATEX, RoHS).
Equipped with over 200 advanced automated production and testing units, our intelligent facilities guarantee batch-to-batch precision and reliable lead times for worldwide telecommunication deployment.
Explore our full line of UL-listed, explosion-proof, multi-hole, and nylon-reinforced cable glands engineered for zero-compromise telecommunication connectivity.